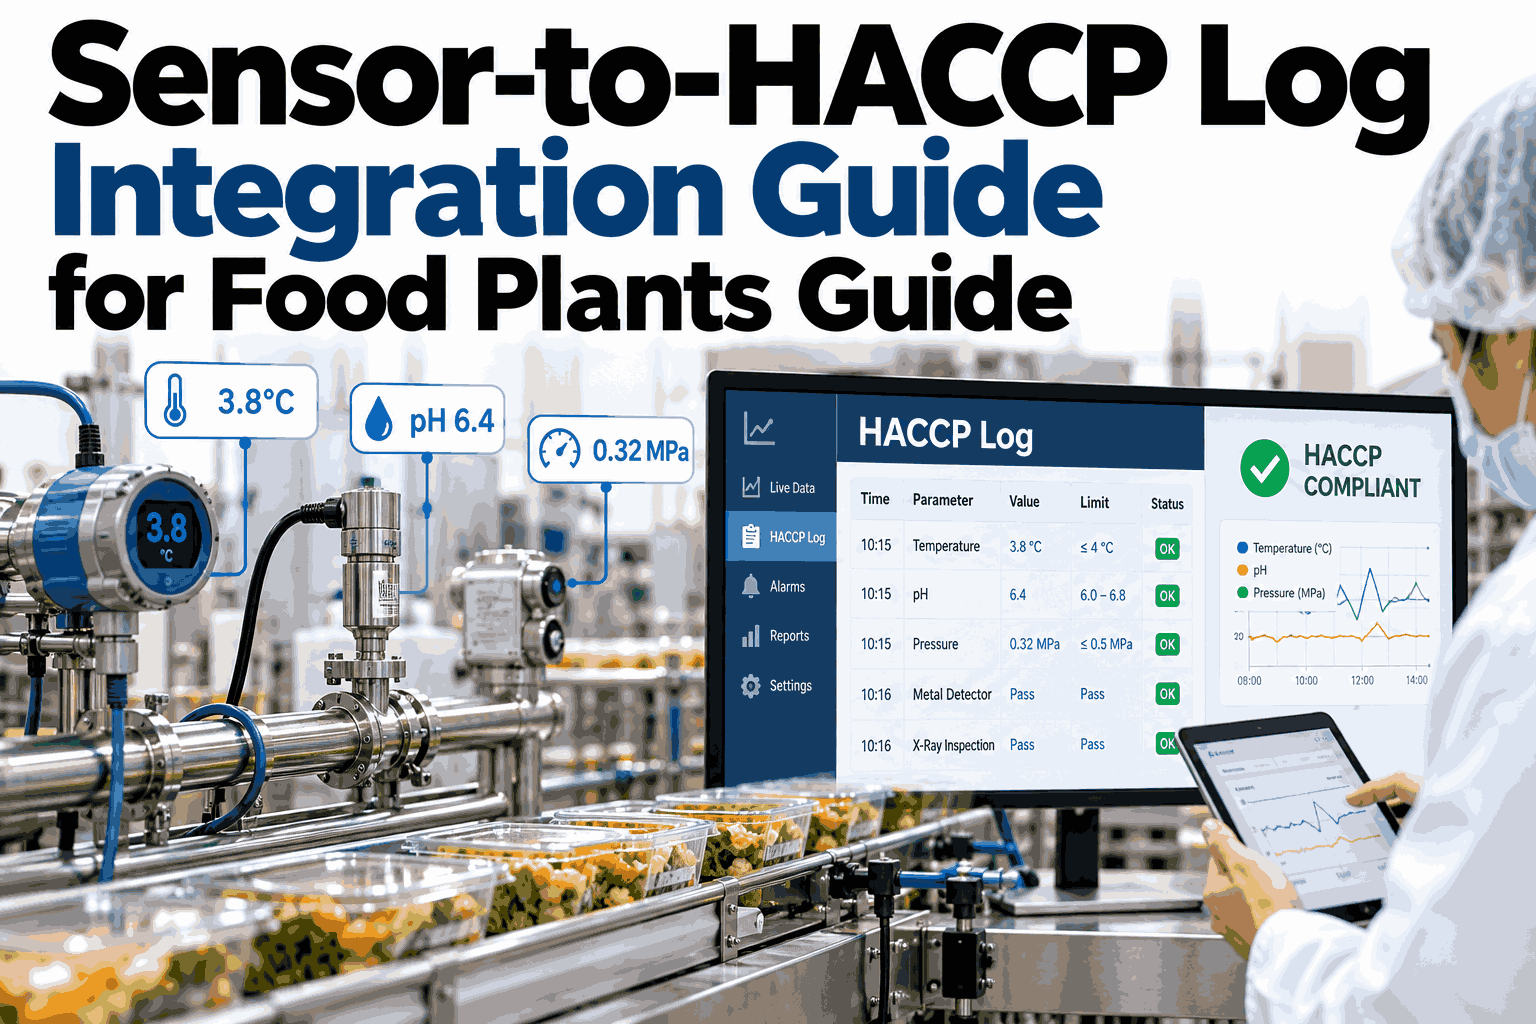
Most food plants still run their Hazard Analysis Critical Control Point program on two systems at once: the sensor that reads the real temperature, and the operator who copies that number onto a paper sheet or into a spreadsheet an hour later. Every re-typed value is a chance for a transcription error, a missed deviation, or a record that does not match what actually happened at the pasteurizer. Plants preparing for an FDA or third-party audit often find the gap between sensor data and the signed HACCP record is exactly where the real risk hides. A direct path from thermocouple to log removes that gap, and teams can see a sensor-to-HACCP mapping built for their own CCPs in a short walkthrough.
Give Every CCP Reading a Straight Path Into the HACCP Record
iFactory AI connects pasteurizer, chiller and cooking sensors directly to the HACCP log, so a temperature reading becomes a signed, audit-ready record without an operator ever re-typing a single value by hand.
Why Manual CCP Logging Still Breaks Down
A clipboard round sounds simple, but it depends on a person being in the right place at the right minute, reading the right number, and writing it down correctly every single time. Busy lines and short-staffed shifts make that hard to guarantee on every shift.
Most plants run several CCPs at once across different parts of the line, and one operator is often responsible for checking all of them on a rotating schedule. When a line speeds up, when a changeover runs long, or when someone calls in sick, the logging round is the first thing that slips, not because anyone is careless but because there is only one person and several places that need watching at the same time.
A missed or late reading is not just a paperwork problem. During an audit, a gap in the record looks the same whether the CCP was actually out of control or simply unwatched for ten minutes, and the plant has to treat it that way too, which often means a wider investigation than the situation actually called for.
Handwriting adds a second layer of risk on top of timing. A number copied from a gauge to a sheet, and later typed from the sheet into a spreadsheet for trending, passes through two chances for a nine to become a seven or a decimal point to land in the wrong place, and neither mistake is visible until someone goes looking for it.
Where This Shows Up on the Plant Floor
Three CCPs carry most of the logging burden in a typical food plant, and each one shows the gap between manual rounds and continuous sensor data in a slightly different way.
Pasteurization Kill Step
Temperature and hold time both have to clear the limit together, and a short dip during a flow rate change or a valve adjustment is easy to miss between rounds, even when the overall batch looks fine on average.
Cook or Thermal Process Step
Internal product temperature can vary across a batch, and a single spot check at one probe location may not reflect what happened at the coolest point of the load, which is the point that actually matters for the kill step.
Cold Storage and Chiller Monitoring
A door left open overnight, a compressor fault or a defrost cycle running long shows up instantly on a sensor feed, but can sit unnoticed for hours until the next scheduled round picks it up.
The Four-Hop Path From Sensor to Signed Record
Direct capture is not one piece of software. It is a short, well-defined chain, and each hop has a specific job to do before the reading becomes part of the official record.
Sensor Reads the Process
A thermocouple, RTD or pressure transmitter already tied to the PLC produces the value the HACCP plan actually cares about, at whatever resolution the instrument was specified to deliver.
Gateway Tags and Time-Stamps It
An OPC UA or similar gateway reads the tag on a fixed interval and attaches a synchronized timestamp, equipment ID and batch context before the value goes anywhere else.
Historian Checks the Limit
The value is compared against the critical limit from the HACCP plan the moment it lands, not hours later during a manual review of the shift's paperwork.
Record Is Written and Signed
A record is generated automatically, with any deviation flagged and linked to the batch it belongs to, ready for the designated person to review and sign off.
None of these four hops requires a new control strategy. The HACCP plan still names the same CCPs, the same critical limits and the same corrective actions, and the plant's validated process does not change at all. What changes is only how the reading travels from the sensor on the floor to the page the auditor eventually reads during an inspection.
| Dimension | Manual Logging | Direct Sensor Capture | Risk Removed |
|---|---|---|---|
| Timing | Rounds every 30 to 60 minutes | Continuous, every few seconds | Short excursions going unseen |
| Transcription | Operator reads gauge, writes number | Value read directly from the tag | Copy and rounding errors |
| Deviation handling | Noticed at next round or review | Flagged the moment it occurs | Delayed corrective action |
| Traceability | Depends on legible handwriting | Tag ID, sensor ID and timestamp attached | Unclear source during investigation |
| Audit prep | Binders pulled and cross-checked by hand | Records queryable by CCP and date range | Days of pre-audit assembly work |
| Shift handover | Verbal notes or a paper logbook entry | Full history visible to the incoming shift | Context lost between shifts |
The table is not an argument for buying new sensors. In most plants, every tag in that right-hand column already exists somewhere in the PLC or SCADA system, reading the process for control purposes. Direct capture simply gives the HACCP record access to a value that was already being measured.
See Your Own CCPs Mapped to a Direct Capture Path
Book a 30-minute session and iFactory AI will show how your pasteurizer, chiller or cooking sensors map onto a signed HACCP record, using data from your own plant rather than a generic demo.
What Counts as Audit-Ready Data
Not every digital number is an audit-ready record. Auditors look for specific qualities in the data itself, not just a clean-looking report, and a spreadsheet typed in after the fact rarely satisfies all of them.
A digital record that cannot show where the value came from, or that can be edited after the fact with no trace of the change, offers little advantage over paper. The five qualities below are what separate a record an auditor accepts without question from one that invites follow-up questions.
A Recall Query, End to End
The real test of any HACCP record system is not a normal day, it is the day a recall question lands on the QA manager's desk and needs an answer within the hour.
Lot Is Identified
A customer complaint or an ingredient alert narrows the question down to a specific lot, line and production date.
Records Are Pulled
Every CCP record tied to that lot is retrieved by date and batch, with no binder to search or handwriting to decipher.
Answer Is Returned
The QA team confirms every critical limit was met for that lot, with timestamps and sensor IDs attached as evidence.
Where This Plugs Into Your Existing Systems
Direct capture does not replace the control systems already running the line. It reads from them and writes into the quality record that sits alongside, which keeps the project scope small compared with a full control system overhaul.
Integration work usually starts with an inventory of which CCPs already have a working sensor on an accessible network, since those are the fastest to bring online. Points that currently rely on a stand-alone gauge with no network connection are mapped separately, and a plan is made for whether a small add-on transmitter makes sense there.
PLC and DCS
Reads existing process tags over the network without changing control logic, ladder code or adding new sensors anywhere on the line.
SCADA Historian
Pulls time-series values already stored for process monitoring and trending, and reuses the same history for compliance reporting.
OPC UA Gateway
Provides a secure, standard interface between plant floor equipment and the HACCP record layer, so new tags can be added without custom point-to-point connections.
MES and ERP
Links each HACCP record to the batch, lot, line and shift it belongs to, so a single record can be pulled up instantly during a recall investigation.
What Changes for the QA Team Day to Day
The job does not disappear, it shifts. Reviewing and signing records is still a human responsibility, but the work moves from chasing data to checking exceptions.
Signals It Is Time to Move Off Manual Logging
Not every plant needs to make this change on the same timeline. A handful of recurring patterns are usually a sign the manual process has reached its limit.
Validation and Calibration Still Matter
Direct capture changes how a reading travels, not whether the reading itself is trustworthy. The instrumentation still has to be calibrated and the process still has to be validated on its own merits.
A sensor that is out of calibration will produce a confident, perfectly timestamped, perfectly traceable wrong number, and an automated system will log it just as faithfully as a correct one. Calibration schedules, verification checks and instrument maintenance stay exactly as important as they were before, and in most plants they remain the responsibility of the same maintenance and QA staff who manage them today.
What changes is that the calibration record itself can be linked to the sensor ID in the HACCP record, so an auditor reviewing a reading can see at a glance when that instrument was last verified and against what standard.
Frequently Asked Questions
Does this replace our existing HACCP plan or paperwork system?
No, it keeps your HACCP plan exactly as validated and simply changes how the record is populated. The critical limits, CCPs and corrective actions you already have stay the same, only the data entry step becomes automatic, so no revalidation of the underlying process is required. Support can walk through how your current plan maps onto direct capture before anything changes.
What happens when a sensor reading shows a real deviation?
The deviation is flagged the moment it is captured and routed to the person responsible for corrective action under your plan. The system does not decide what to do about it, it simply makes sure the deviation cannot be missed or logged late. Your documented corrective action procedure still applies in full, and the flagged record becomes part of the evidence that the procedure was followed.
Can an auditor trust a digital record over a signed paper sheet?
Auditors generally trust records more when the chain from sensor to record is documented and tamper-evident, which is harder to prove with a signed paper sheet that anyone could have filled in later. Timestamp precision, sensor traceability and immutability matter more than whether the record is printed or digital. See how a direct capture record is structured for your own audit requirements.
What sensors and equipment can connect without new hardware?
Most plants already have thermocouples, RTDs and pressure sensors wired into a PLC or SCADA system, and those existing tags are what direct capture reads. New sensors are only needed where a CCP currently has no instrumentation at all, which is uncommon on an established line that already relies on these readings for process control.
How long before our QA team sees value from this?
Tag mapping and critical limit configuration typically take the first few weeks, with signed automatic records live well inside the 12-week rollout. Many teams see the first reduction in missed or late readings as soon as the gateway starts reading tags, well before every CCP on the line is fully mapped. Ask support what a realistic timeline looks like for your specific CCPs.
Close the Gap Between the Sensor and the Signed Record
iFactory AI turns existing CCP sensors into audit-ready HACCP records, with no operator re-typing a single value and no gap between the reading and the record. Book a walkthrough to see it on your own line.
A pasteurizer holds 161°F for the required dwell time, but the number that ends up on the CCP log is whatever an operator reads off the gauge and writes down on the next walk-through, sometimes two or three minutes after the moment it actually mattered. That gap between what the sensor measured and what the paper record says is where most HACCP data integrity problems start, and it is also the gap a direct sensor-to-record path is built to close. A thermocouple that writes straight into a signed, time-stamped CCP record removes the re-typing step entirely, and plants that want to see that path running against their own pasteurizer or retort can walk through a live sensor-to-record connection in a short session.
Get the Reading Straight From the Sensor to the Signed Record
iFactory AI reads CCP sensors directly, time-stamps every value, and writes it into the HACCP record without an operator re-typing a number from a gauge.
Where Manual CCP Monitoring Actually Breaks Down
Paper logging is not careless, it is just structurally slow in three specific places, and each one is a point where the written value can drift from what the sensor actually measured.
Reading-to-Writing Lag
The temperature an operator writes down is whatever the gauge shows at the moment of the walk-through, not necessarily the lowest point during the dwell time.
Transcription Drift
A value moves from clipboard to spreadsheet to binder, and each transfer is a chance for a digit to be copied wrong or a reading to be back-filled from memory.
Gaps Between Checks
A fixed check interval, such as every 30 minutes, means a short excursion between checks can come and go without ever reaching the paper record.
What a Regulator Actually Checks in an Electronic Record
Electronic HACCP records are judged against the same data integrity principles that apply to any regulated record: who made it, when, and whether it was changed afterward.
| Principle | What It Means for a CCP Record | Risk If Missing |
|---|---|---|
| Attributable | The record shows which sensor and which operator or system produced the value | A disputed reading cannot be traced to its source |
| Contemporaneous | The value is recorded at the time it was measured, not reconstructed later | Back-filled entries look identical to real-time ones on paper |
| Original | The first captured value is preserved, not a transcription of it | A copying error becomes the official record |
| Accurate | The value matches what the sensor actually measured, within calibration tolerance | A misread gauge produces a false pass or false fail |
A direct sensor-to-record path satisfies all four by construction, because there is no human transcription step between the measurement and the stored value for an auditor to question.
The Path From Thermocouple to Signed Record
Four hops stand between a sensor and a usable HACCP record, and skipping or weakening any one of them is where most "automated" logging projects quietly fall short.
See This Path Built Against Your Own Pasteurizer
Book a 30-minute session and iFactory AI will walk through reading a real CCP sensor and writing it to a time-stamped record.
Matching the Protocol to What's Already on the Floor
Most food plants are not starting from a blank slate. The right integration approach depends on what the existing controls on a pasteurizer, retort, or chiller already speak.
| Equipment Age | Typical Interface | Integration Approach |
|---|---|---|
| Modern PLC/SCADA | OPC-UA or a documented Ethernet protocol | Direct tag read, usually no controller changes needed |
| Older PLC | Modbus RTU or TCP | Gateway translation into the historian without touching ladder logic |
| Standalone chart recorder | No network interface | A retrofit sensor tap or a validated digital replacement |
| Manual gauge only | No electronic signal at all | A calibrated sensor and transmitter added at the CCP |
A plant with a mix of all four is common, and the integration project usually tackles the modern equipment first, since it typically requires no physical changes to the control panel.
What Happens When a Reading Crosses the Limit
A direct feed does more than log a number, it can evaluate that number against the CCP limit the instant it arrives, which changes how a deviation gets handled.
Within Limit
Out-of-Limit
An Illustrative Comparison: Pulling a Record During an Audit
The figures below are a labeled illustrative composite, not a reported customer result, showing how record retrieval time can change once logging moves off paper.
Results vary by plant and by how many CCPs are still on paper versus already instrumented. The direction holds consistently: removing the transcription step removes most of the disputes about what a record actually says.
Where iFactory AI Fits
iFactory AI is smart manufacturing and industrial software built to connect existing plant sensors to the records that depend on them, without requiring a rebuild of the control system underneath.
Direct Sensor Reads
CCP sensors are read through OPC-UA, Modbus, or a gateway, without a manual re-entry step anywhere in the path.
Real-Time Limit Checking
Every value is compared against the CCP limit as it arrives, flagging a deviation the moment it occurs.
Signed, Time-Stamped Records
Each reading is written into a record attributable to its sensor and source, satisfying the core integrity principles auditors check.
Lot-Level Traceability
CCP records are tied to the lot in production at the time of the reading, so retrieval during an audit or a hold decision is immediate.
Frequently Asked Questions
Does this replace our HACCP plan or just how it's logged?
It only changes how CCP monitoring is captured and recorded, not the HACCP plan itself, including the limits, the monitoring frequency, and the corrective actions your plan specifies. The plan stays exactly as validated, with the sensor feed simply replacing the manual transcription step. Review how this fits around your existing HACCP plan in a short walkthrough.
What happens if a sensor fails or loses connection?
A connection loss is itself logged as an event, and most plants keep a documented fallback to manual monitoring for that CCP until the sensor or connection is restored, exactly as a validation plan would require. The gap is visible in the record rather than silently missing. Ask the iFactory AI team how failover is handled for your specific equipment.
Do older pasteurizers and retorts need new sensors to do this?
Not always. Equipment with an existing PLC or chart recorder output often already has a usable signal that can be read through a gateway without touching the control logic, while equipment with only a manual gauge does need a calibrated sensor added at the CCP. Get an assessment of your specific equipment on a 30-minute call.
How does this hold up during a regulatory audit?
Records are attributable to the sensor and timestamped at the moment of capture, which directly addresses the data integrity questions an auditor typically raises about paper logs, such as who recorded a value and when. Retrieval for a specific lot is also far faster than searching a binder. See a sample audit retrieval on your own lot data in a demo.
Can this integrate with the ERP or quality system we already use?
Yes, CCP records and lot data are built to feed existing ERP, MES, or quality management systems rather than living in a separate silo, so hold decisions and lot release can happen from the systems your team already works in. Talk through your current system landscape with the iFactory AI team.
Put the Sensor Between the CCP and the Record, Not the Clipboard
iFactory AI reads your CCP sensors directly and writes signed, time-stamped records with no manual re-entry. Book a walkthrough built around your own pasteurizer or retort.